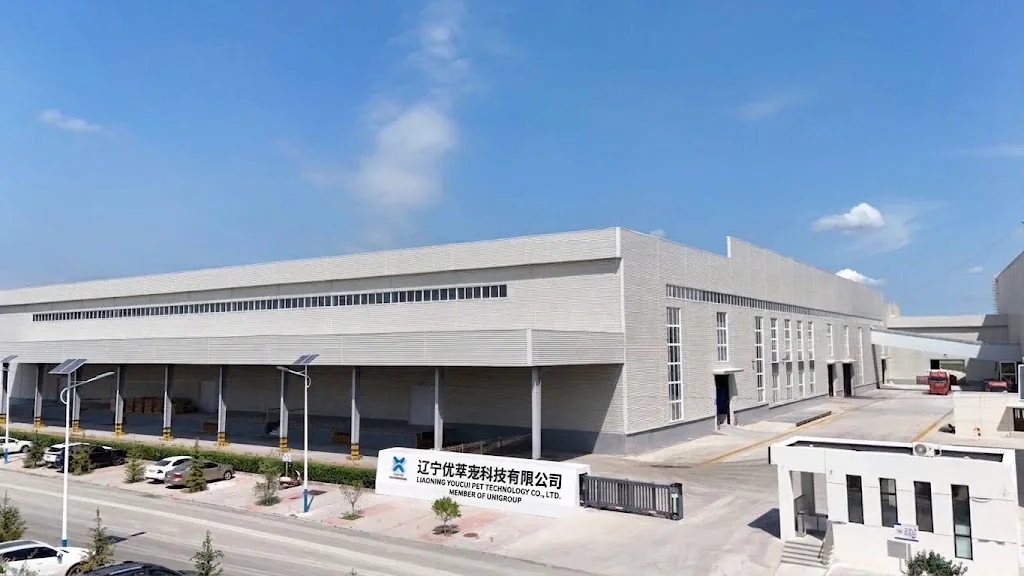
ULTREX PET (LIAONING) TECHNOLOGY DEVELOPMENT CO., LTD.
From Mine
to Pack.
A full-process field inspection of our bentonite cat litter operation—from mineral extraction and wet sodium activation to dust control, laboratory testing and export-ready packing.
80M tHigh-grade reserves
150 daysNatural aging
≤1%Dust target
00
FIELD INSPECTION OVERVIEW
Premium mineral quality, engineered for consistent cat litter performance.
High-end bentonite cat litter begins with the right mineral deposit, but raw material alone is not enough. Ultrex Pet (Liaoning) combines an integrated mineral supply, proprietary wet sodium activation and an intelligent production system to control performance from source to shipment.
This inspection follows six critical stages: raw ore, modification, dust control, finished-product testing, automated packing and smart warehousing.
01
SOURCE INSPECTION
THE QUALITY FOUNDATION
Integrated mineral supply starts consistency at the source.
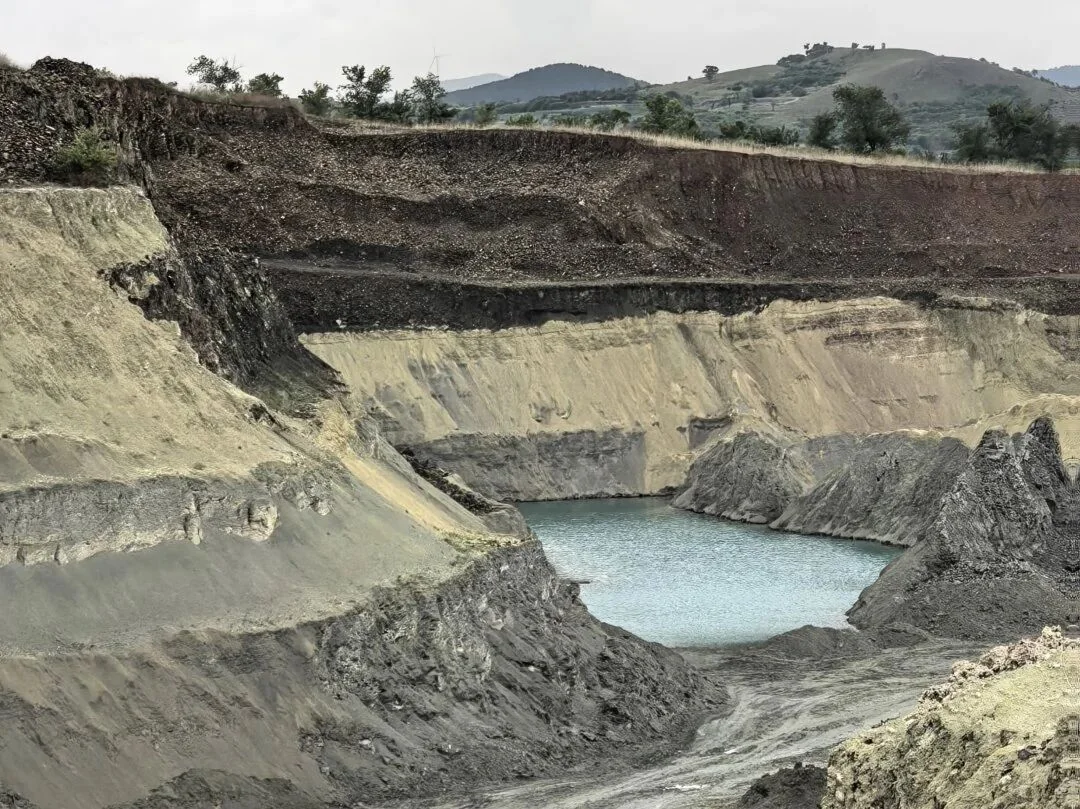
Our parent company's open-pit mine contains a reported 80 million tonnes of high-grade bentonite reserves—sufficient for approximately 80 years of stable extraction at the planned operating rate.
Low impurity, strong activity
Raw ore is selected for less than 5% sand content, continuous mineral veins and strong montmorillonite activity.
Every load is sampled
Montmorillonite content is controlled at 40% or above before the ore enters the processing sequence.
Protection after screening
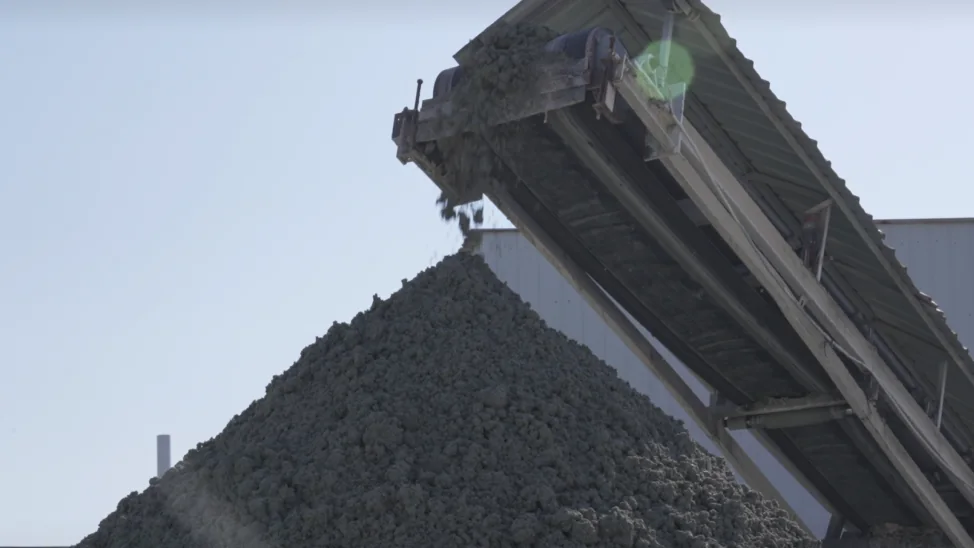
Crushed and screened material moves to storage through enclosed transfer, reducing secondary contamination and dust.
02
CORE PROCESS
WET SODIUM ACTIVATION
Deep modification creates the performance difference.
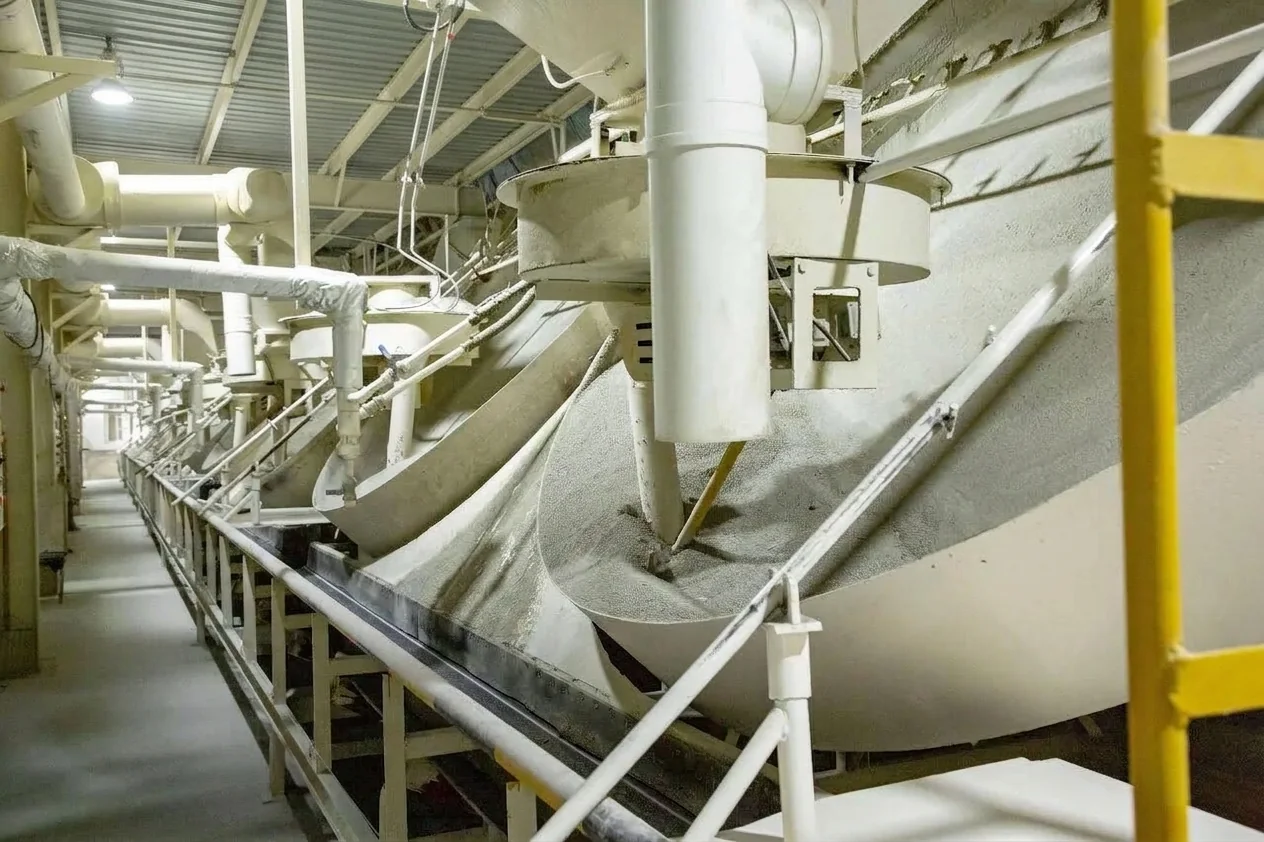
The RMB 200 million intelligent facility uses a proprietary wet sodium activation route. Unlike dry solid-state mixing, the wet process promotes more uniform ion exchange throughout the bentonite structure.
Slurry preparation
Crushed ore is blended into a controlled-concentration slurry.
Uniform reaction
Liquid–solid contact enables deeper sodium-ion exchange than surface-only mixing.
Digital monitoring
Concentration, temperature, pH and residence time are monitored centrally.
Multi-pass pressing
Modified slurry is repeatedly rolled and formed into conditioning cakes.
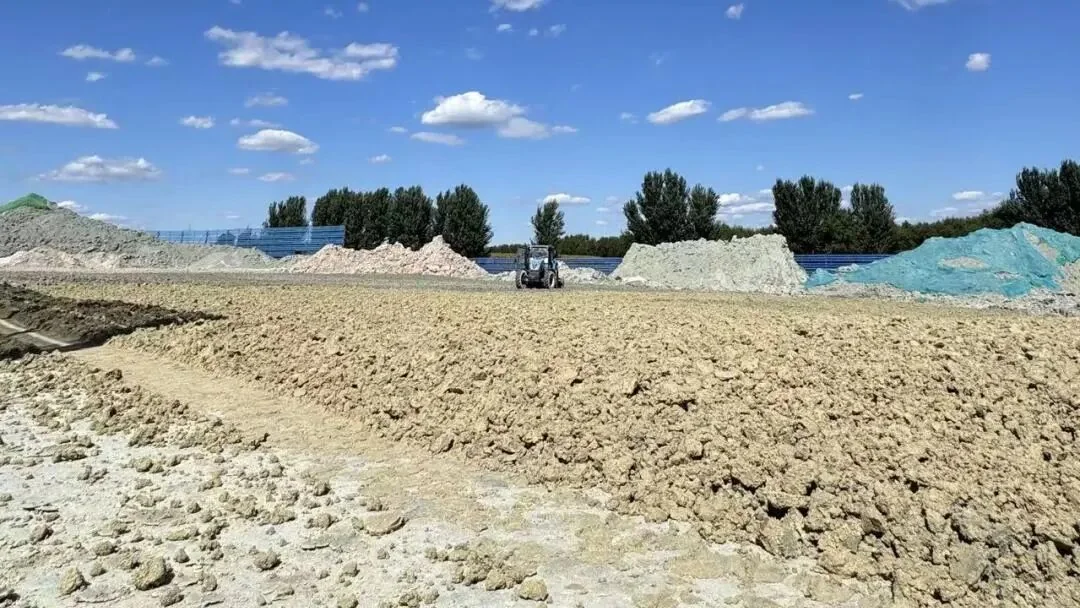
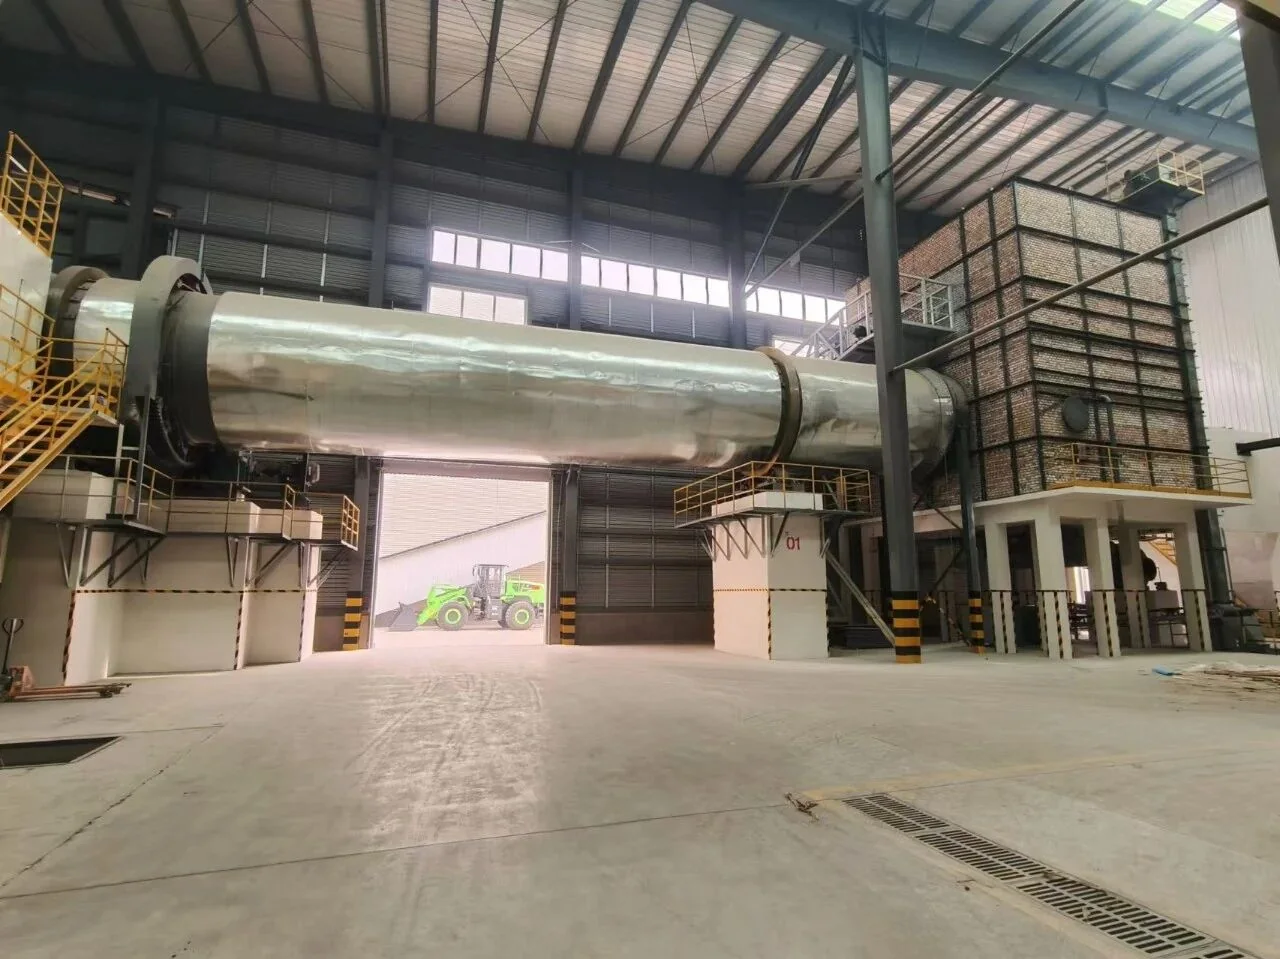
32-MU CONDITIONING AREA
150 days of natural aging.
Extended aging allows the activation reaction to stabilize. The process is designed to reduce reverse ion exchange, soft clumps, sticking and inconsistent dust performance.
≥90%Reported wet-process sodium activation rate
03
PROCESS CONTROL
LOW-DUST ENGINEERING
Dust control is designed into the line—not added at the end.
A closed-loop screening system and final negative-pressure extraction cover 14 production points, from crushing and granulation to final classification.
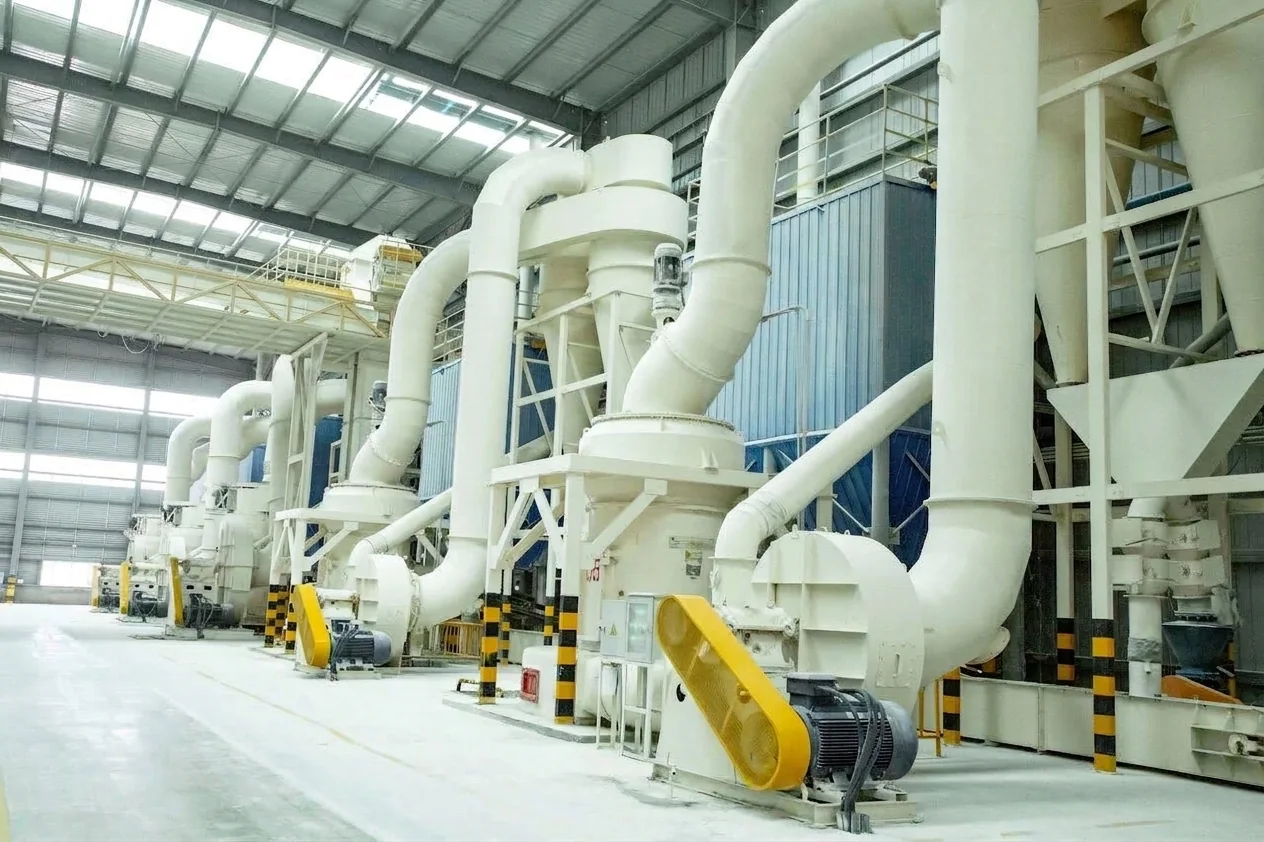
Oversized particles return to the line for controlled reprocessing, while fine airborne material is captured continuously. Routine sampling confirms that each stage remains within its operating target.
04
QUALITY ASSURANCE
BATCH-BY-BATCH VERIFICATION
Every finished batch is tested, recorded and traceable.
The facility supports spherical, crushed and blended bentonite litter across more than ten configurations. A CNAS-accredited testing and R&D center verifies both immediate performance and storage stability.
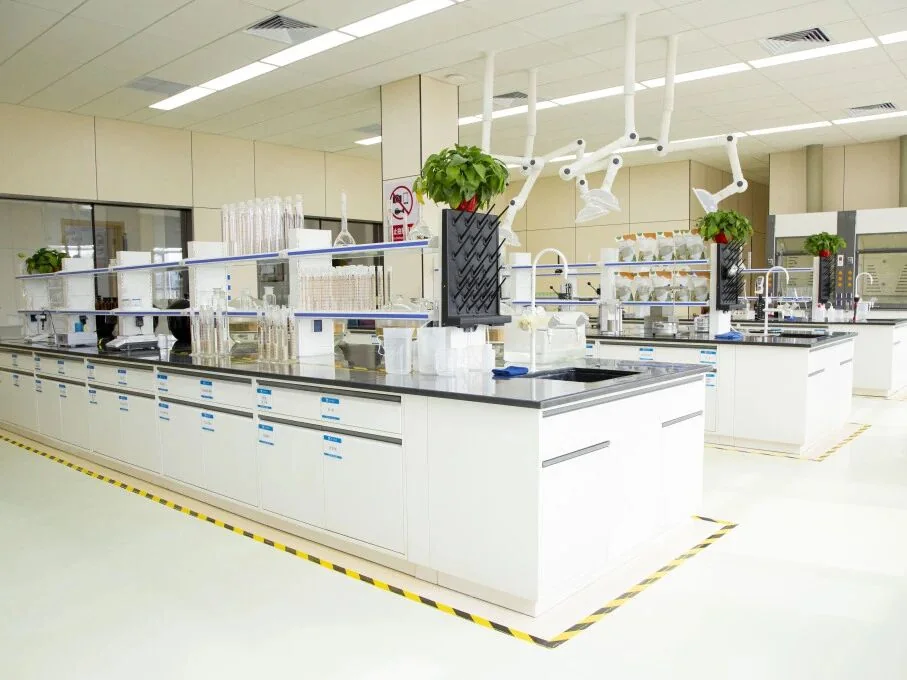
CORE BATCH TESTS
Absorption
Clump strength
Odor control
Dust rate
Sodium activation
Storage stability
Digital traceability
Process records connect raw material, operating parameters, inspection results and finished goods. Any deviation can be traced back to its production stage and batch.
05
PACKING & DELIVERY
THE FINAL CONTROL POINT
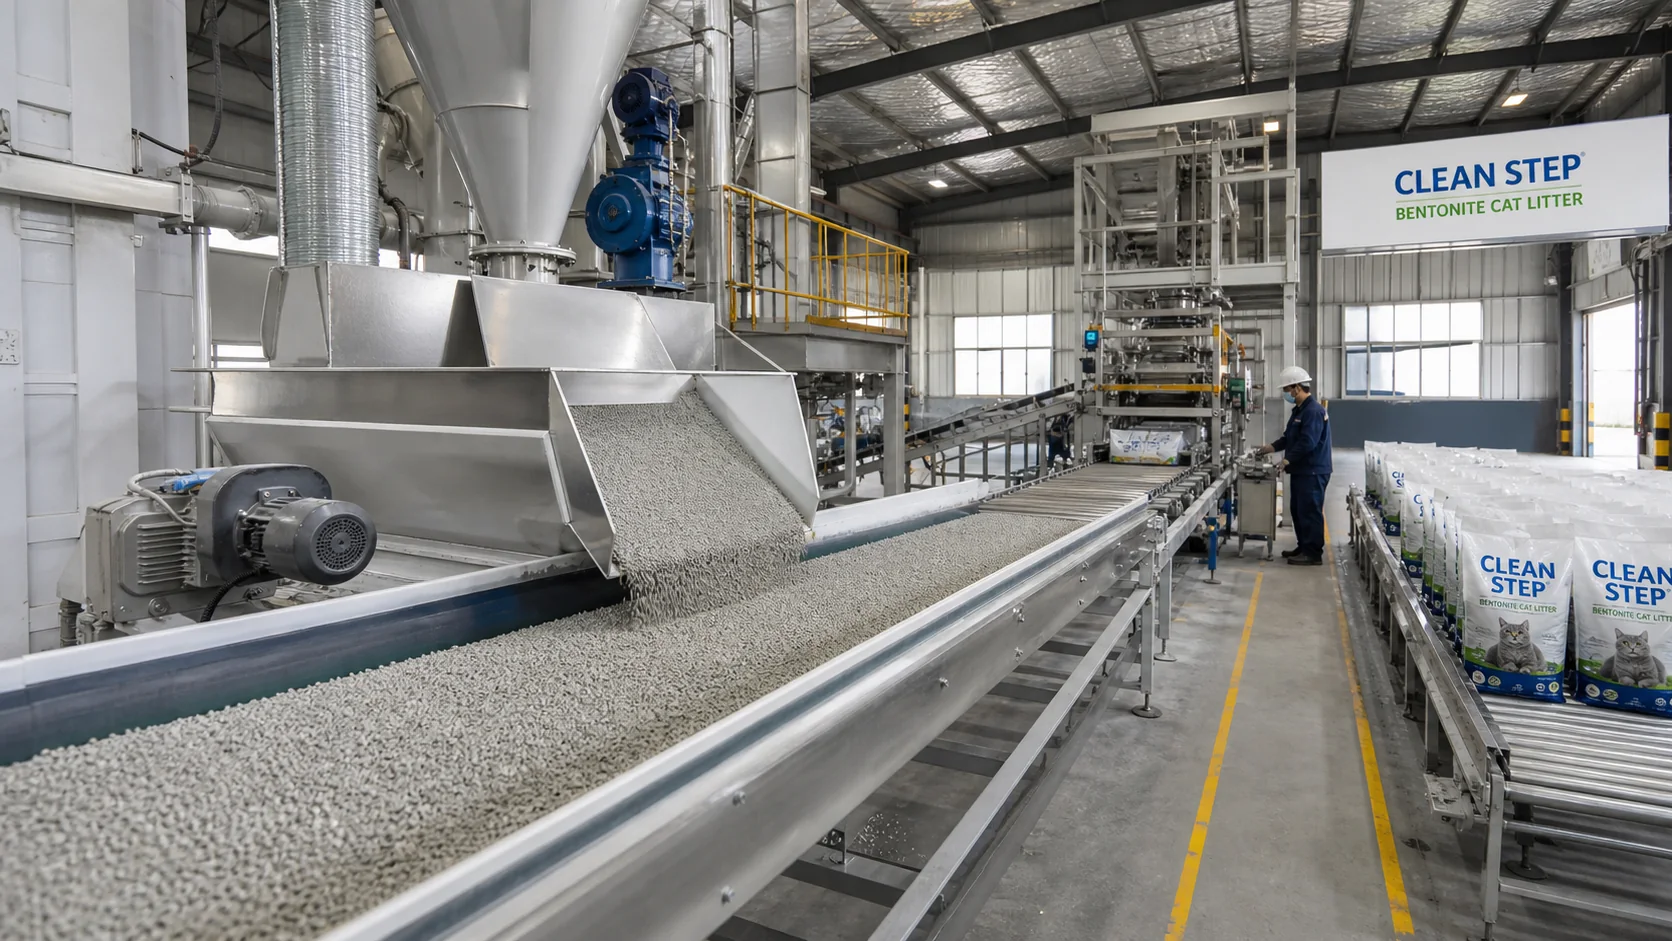
Automated packing protects product integrity through shipment.
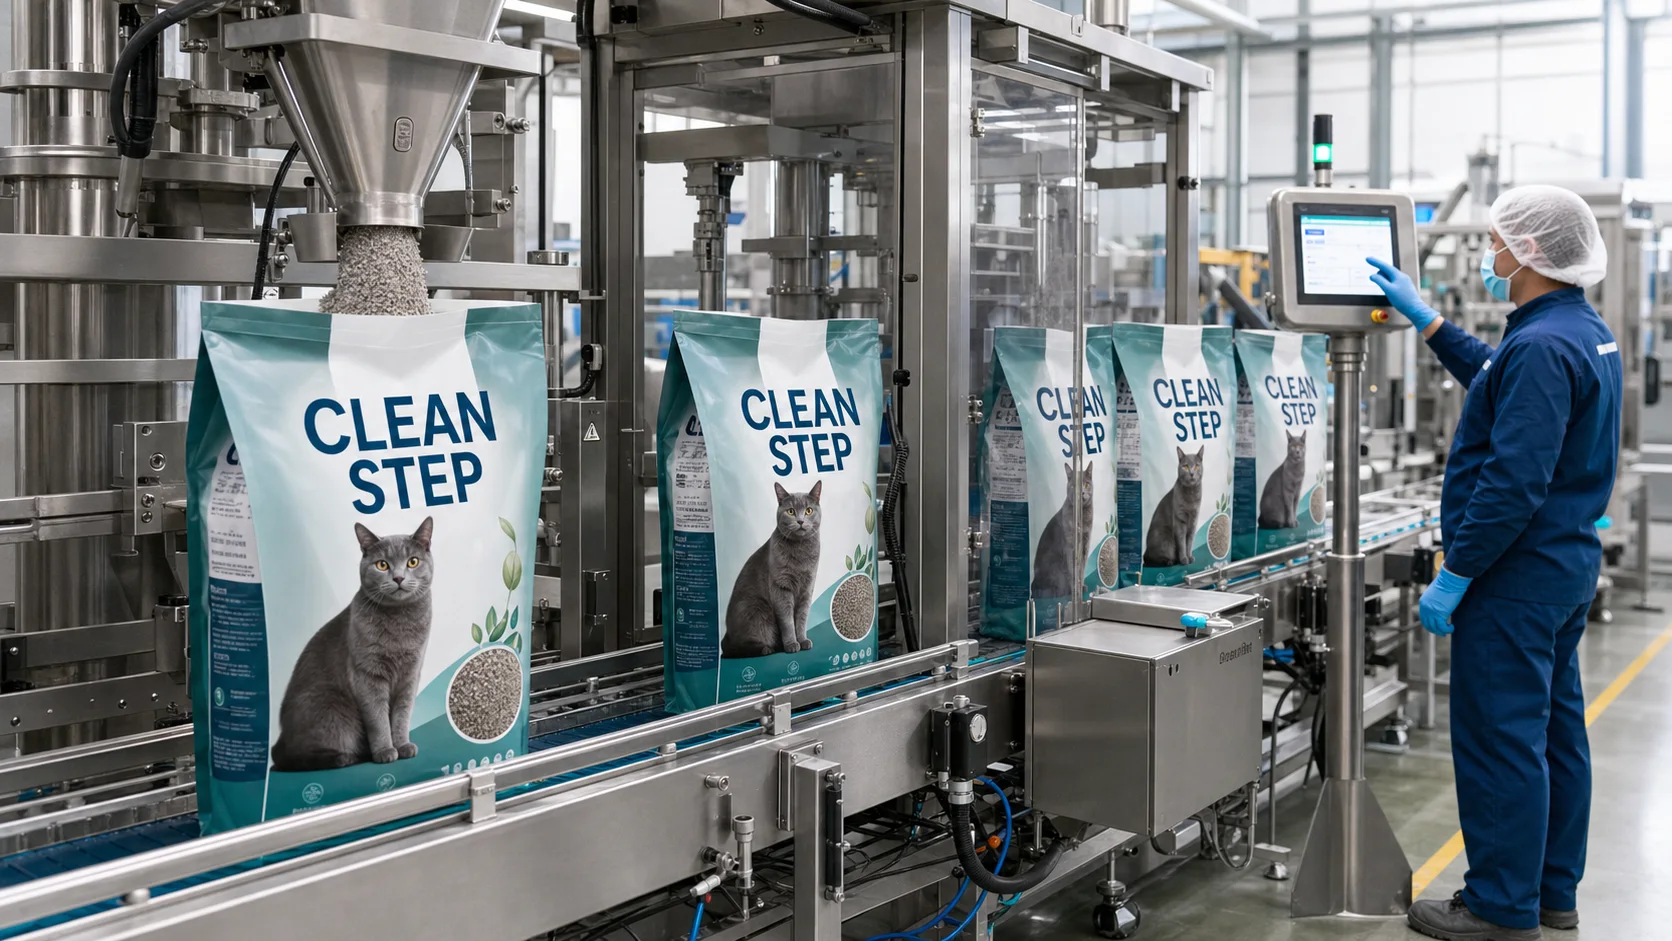
Sixteen automated lines handle weighing, filling, sealing, coding and palletizing. Configurations can be adapted for retail, private-label and export programs.
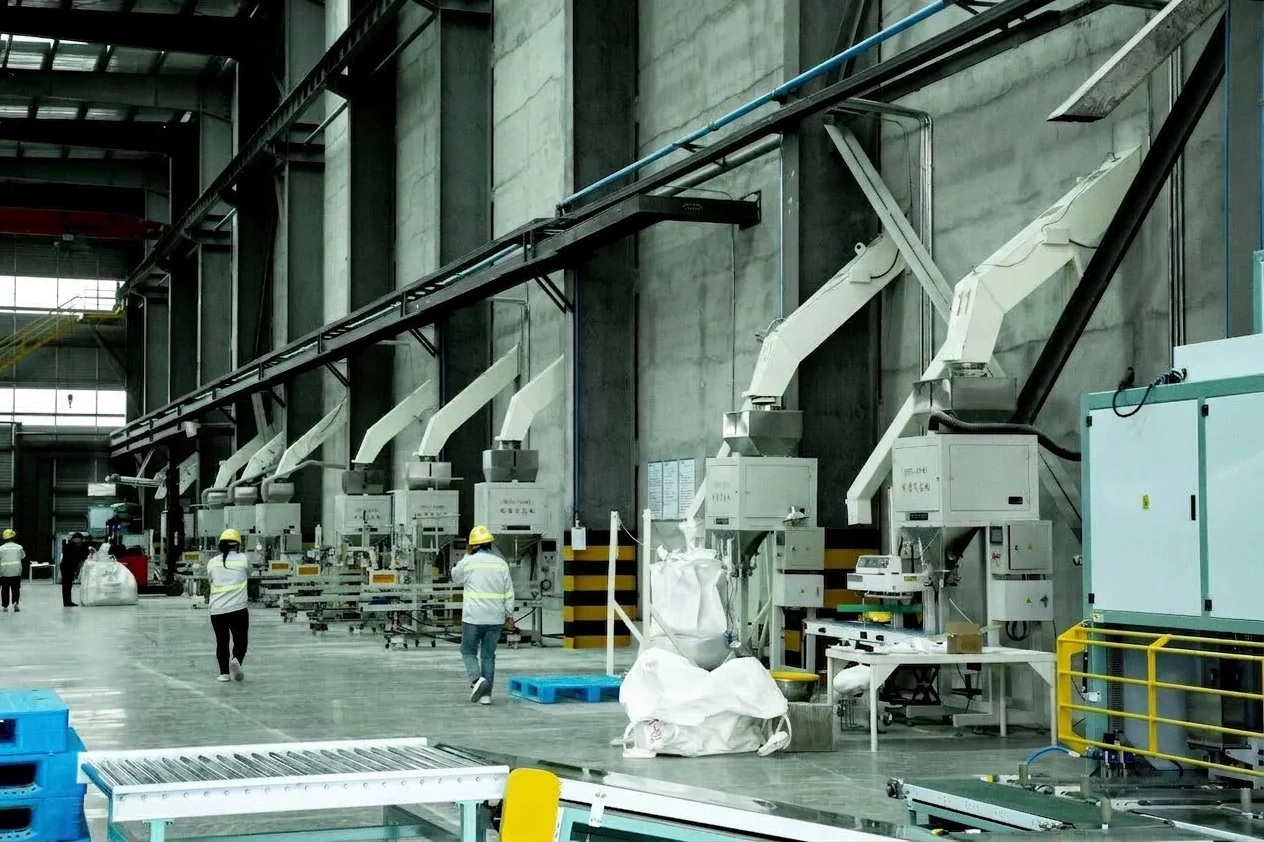
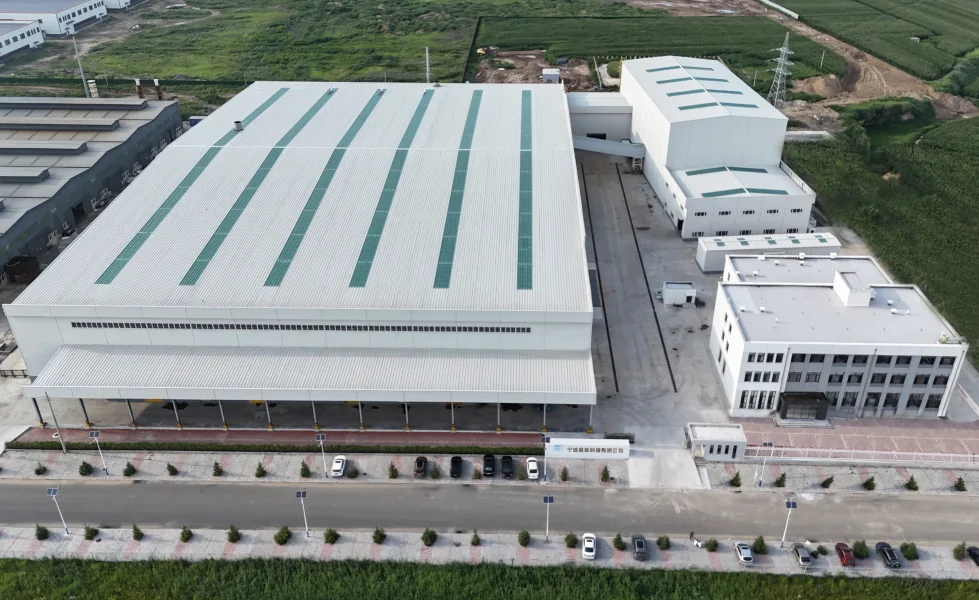
Smart warehousing
Zoned storage with temperature, humidity and ventilation monitoring helps prevent moisture regain and caking.
Pre-shipment sampling
Seal integrity and granule condition are checked before finished goods are released.
Global programs
OEM/ODM development, customized packaging and international logistics support are available for qualified partners.
06 · INSPECTION SUMMARY
Quality is a chain. Every link is controlled.
From mineral selection and wet sodium activation to 150-day aging, low-dust processing and full-batch verification, Ultrex Pet (Liaoning) builds consistency into every production stage.
As a drafting participant in China's bentonite cat litter group standard and a chair organization in the cat litter industry association, the company continues to develop lower-dust and next-generation functional products for global partners.
Discuss Your Specification